Hydrofluoric Acid‑Resistant Anticorrosive Coating
Based on modified phenol‑fluorine resin and polyhydroxy ester as composite base materials, compounded with a special hydrocarbon wax additive system, precisely proportioned with isocyanate component via chemical formulation, a high‑performance coating system with interpenetrating network structure is constructed through molecular design.It features great properties as:
Hydrofluoric Acid‑Resistant Anticorrosive Coating Basic Technical Datasheet
Color
|
Grey |
Gloss |
Flat or Gloss |
Density |
~1.47 Kg/L (after mixing) |
Curing Agent |
Special dedicated curing agent |
Solid Volume |
(98±2) % |
| Standard Film thickness |
200 μm dry film thickness (about 205 μm wet film thickness) |
| Theoretical spreading rate |
4 m²/Kg (at 200 μm dry film thickness) |
| Full cure |
7d at (23±2℃) |
| Flash Point |
57℃ |
 |
Hydrofluoric Acid‑Resistant Anticorrosive Coating Product Packaging
Packaging: Part A :17kg in a 20-liter iron bucket. Part B :10kg in a20-liter iron bucket. Shelf Life:
12 months If exceeding shelf life, the products shall be tested before using.
|
Hydrofluoric Acid‑Resistant Anticorrosive Coating Applicable Environment
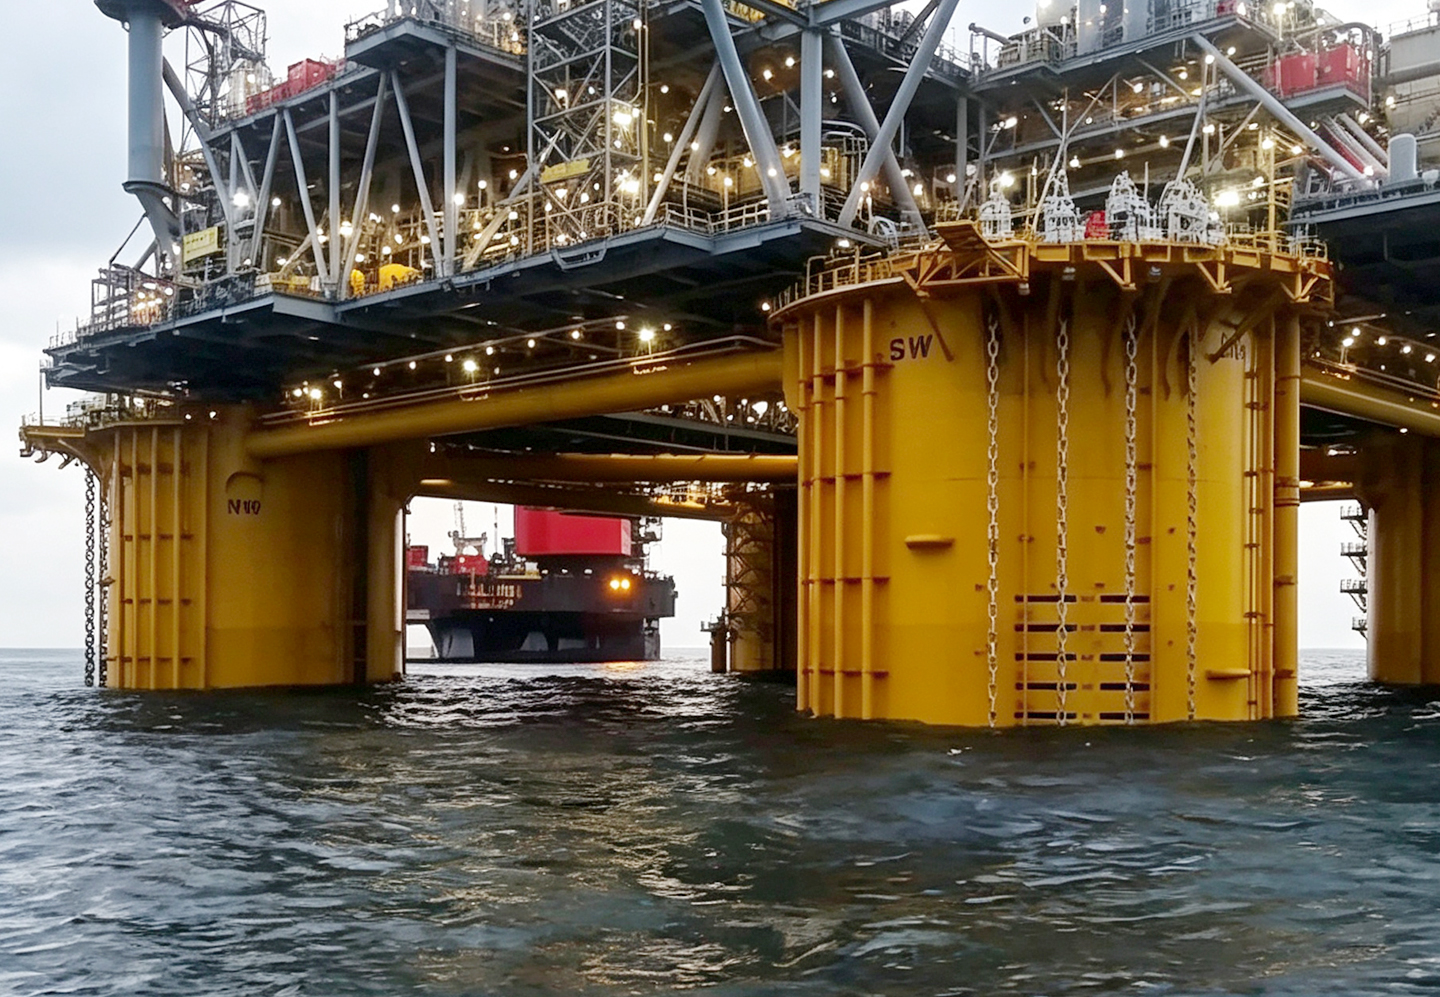 | 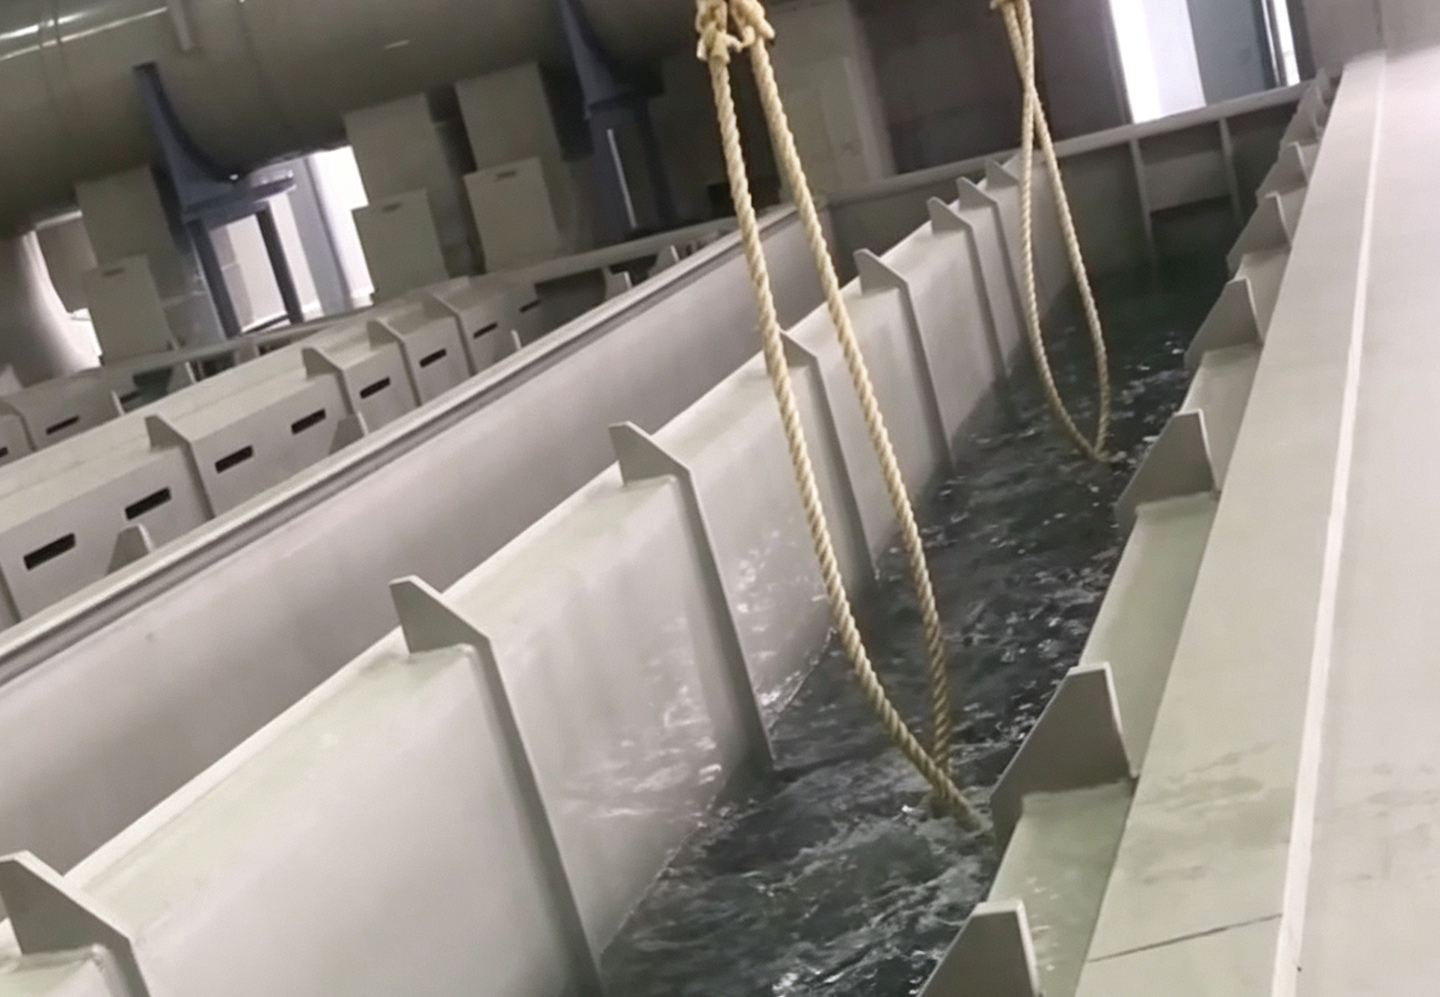 | 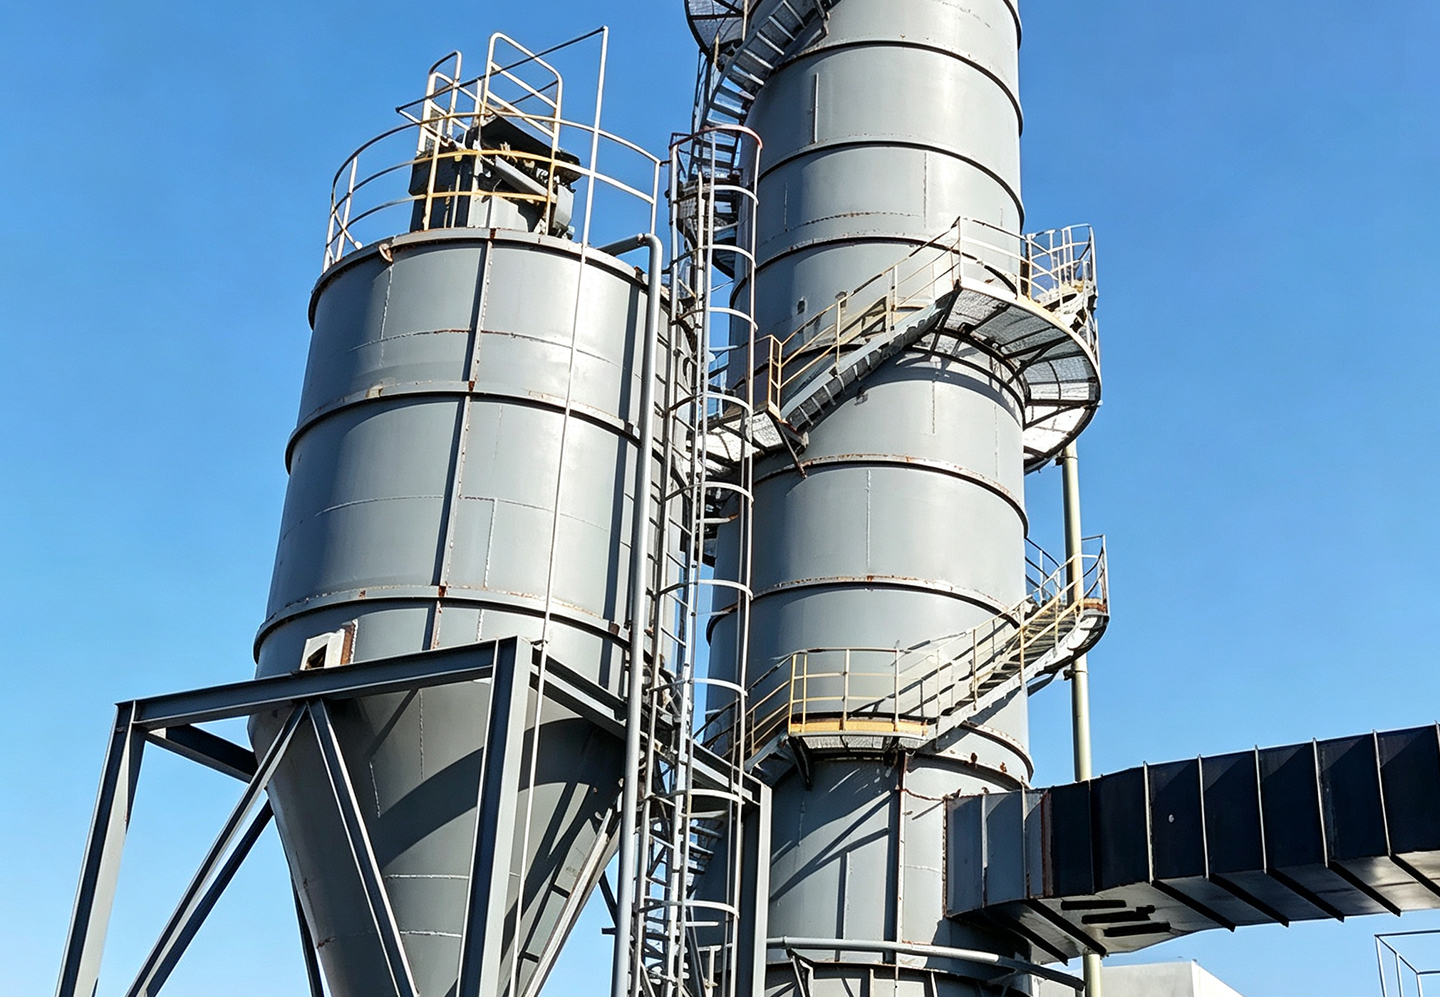 | 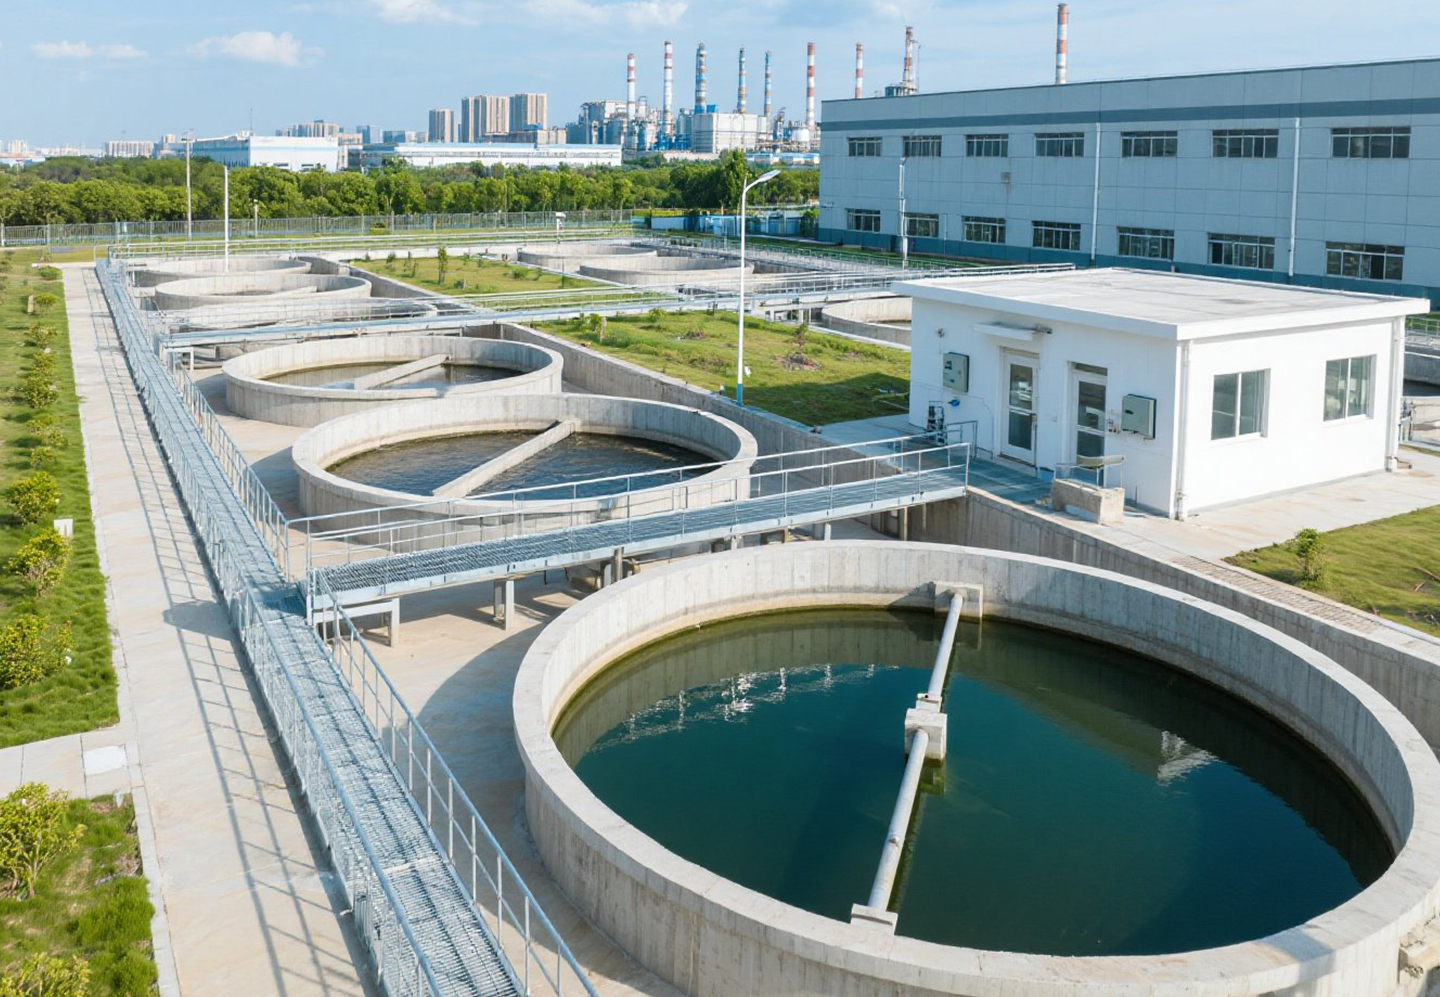 |
| Cross-sea bridges |
Port terminals | Tunnels | Basements |
Hydrofluoric Acid‑Resistant Anticorrosive Coating Finished Projects
Hydrofluoric Acid‑Resistant Anticorrosive Coating Production Process
Hydrofluoric Acid‑Resistant Anticorrosive Coating Instructions For Use
Substrate Treatment:
All surfaces to be coated shall be clean, dry and free of contaminants. Surfaces shall be assessed and prepared in accordance with ISO 8504.
Bare steel: Blast‑clean to Sa 2.5 (ISO 8501‑1:2007). For non‑immersed service environments, power‑tool cleaning may be acceptable, provided that a minimum grade of St 2 (ISO 8501‑1:2007) is achieved.
Stainless steel surfaces shall be mechanically or hand‑abraded using non‑metallic abrasives, fibre pads or hand sandpaper to create a textured rough surface; ensure no smooth areas remain.
Galvanized steel surfaces shall be clean, dry and possess adequate surface roughness.
Instructions for Use:
Mixing:
Stir the base component thoroughly with a power mixer, then add the curing agent while continuously stirring until fully homogenous.
Mixing Ratio:
Base Component : Curing Agent = 2 : 1 (by weight)
Thinner: Special Thinner
Airless spray:
Nozzle tip: 0.025~0.031 inches
Spray pressure: 18‑22 MPa
Note: Not suitable for small‑size low‑pressure spray units.
Brush, Roller : Recommended only for pre‑coating and small‑area application, and the required dry‑film thickness must be achieved.
Hydrofluoric Acid‑Resistant Anticorrosive Coating Company Introduction
Hydrofluoric Acid‑Resistant Anticorrosive Coating Exhibitions

 English
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 አማርኛ
 ພາສາລາວ
 ភាសាខ្មែរ
 Bahasa Melayu
 ဗမာစာ
 தமிழ்
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Հայերեն
 עברית
 Latine
 Dansk
 Shqip
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 Oʻzbekcha
 Беларуская мова
 Basa Jawa


